 EN
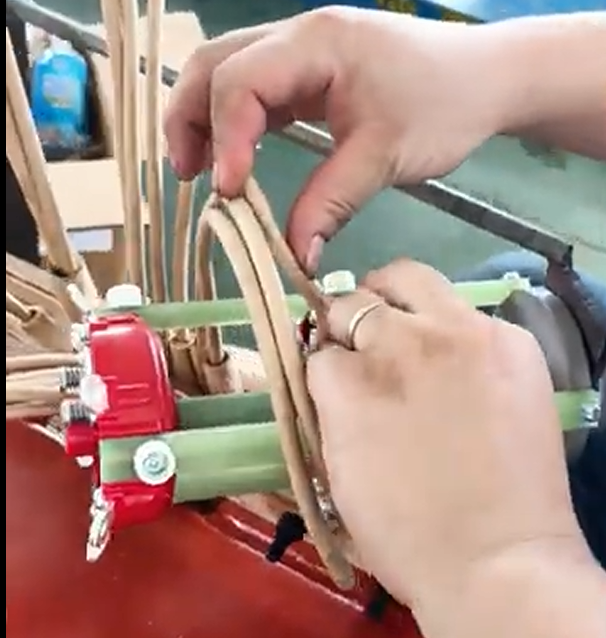
Transformer core stacking is the controlled assembly of thin, insulated electrical steel laminations into the magnetic circuit of a transformer. Lamination material, joint geometry, cutting accuracy, insulation integrity and clamping quality can all affect no-load loss, excitation current, noise and long-term reliability.
In practical transformer manufacturing, there is no single stacking specification suitable for every design. Lamination thickness, step-lap sequence, clamping pressure and inspection limits should follow the approved engineering drawings, material data and applicable testing standards.
Why Is Transformer Core Stacking Important?
The transformer core provides a low-reluctance path for magnetic flux between the windings. Poorly cut or incorrectly stacked laminations can create:
- Uneven air gaps
- Localized magnetic saturation
- Higher excitation current
- Increased no-load loss
- Additional vibration and noise
- Interlaminar short circuits
- Local overheating
Accurate stacking helps maintain the designed magnetic path while protecting the insulation coating on each lamination.
Four Main Steps in Transformer Core Stacking
1. Prepare the Stacking Area
Before assembly begins, the stacking platform, tools and fixtures should be clean, level and free from metal particles, oil and other contamination.
Each electrical steel lamination should be checked for:
- Correct dimensions and cutting angle
- Excessive burrs or sharp edges
- Surface contamination
- Damaged insulation coating
- Bending or deformation
- Correct identification and batch information
Flatness and dimensional tolerances must follow the approved transformer design. A value such as 0.02 mm may be used for a particular component or production process, but it should not be treated as a universal requirement for every transformer core.
2. Stack the Laminations in the Specified Sequence
The laminations are positioned layer by layer according to the core drawing. Many power transformers use an interleaved mitred or step-lap joint to distribute the joint area across several layers.
Operators must control:
- Lamination orientation
- Joint overlap
- Step dimensions
- Layer sequence
- Limb and yoke alignment
- Core window dimensions
- Accumulated stack height
Some production instructions may require the stacking pattern to change after a defined number of sheets. However, a rule such as changing direction every five laminations is design-specific rather than an industry-wide requirement.
3. Align and Pre-Compress the Core
Temporary fixtures are used to hold the stacked core in position before final clamping. Fixtures contacting the electrical steel should avoid scratching or bridging the lamination insulation.
Pre-compression should be:
- Evenly distributed
- Sufficient to stabilize the core
- Applied without deforming the laminations
- Controlled according to the approved process specification
A pressure range such as 3–5 kgf/cm² may apply to a particular factory procedure, but the correct value depends on the core structure, fixture design, material and transformer specification.
4. Inspect the Core and Its Insulation
After stacking and clamping, the core should be inspected before it is assembled with the windings.
Typical checks include:
- Overall core dimensions
- Core window dimensions
- Limb alignment and straightness
- Joint position and gap consistency
- Stack height and filling factor
- Clamping condition
- Core-to-frame insulation
- Core grounding arrangement
- Evidence of interlaminar damage
An insulation resistance value above 10 MΩ may be specified for certain test points or products, but it is not a universal acceptance criterion for all lamination layers. Test voltage, measurement location, temperature, humidity and acceptance limits must be defined by the manufacturer’s procedure and the applicable specification.
How to Select Electrical Steel Laminations
Grain-oriented electrical steel is widely used in power and distribution transformer cores because its magnetic properties are optimized in the rolling direction.
Selection should consider:
- Specific core loss
- Magnetic permeability
- Saturation characteristics
- Lamination thickness
- Insulation coating
- Flatness
- Cutting performance
- Burr characteristics
- Supplier consistency
Comparison of Common Lamination Thicknesses
| Thickness | General characteristics | Selection considerations |
|---|---|---|
| 0.23 mm | Can support lower eddy-current loss, depending on the steel grade | Higher material and processing cost; often selected for demanding loss targets |
| 0.27–0.30 mm | Common balance between performance, availability and cost | Widely considered for power-frequency transformer designs |
| 0.35 mm | Economical for some conventional applications | Core-loss requirements must be evaluated carefully |
| 0.50 mm | Greater potential eddy-current loss | Generally unsuitable for modern low-loss power-transformer cores unless justified by a specific design |
Thinner laminations can reduce the eddy-current component of core loss, but thickness alone does not determine performance. Steel grade, flux density, joint design, cutting quality and assembly accuracy are also important.
Claims such as “0.23 mm steel reduces eddy-current loss by 40%” should only be published when supported by tests conducted under defined and comparable conditions.
Why Material Batch Consistency Matters
Using electrical steel from the same approved grade and controlled production batch helps maintain consistent:
- Magnetic properties
- Sheet thickness
- Insulation coating performance
- Surface condition
- Cutting response
- Core build dimensions
Mixing unidentified materials can create inconsistencies in core loss, excitation current and stacking dimensions. If multiple batches must be used, they should be verified through material records and the manufacturer’s quality-control process.
Three Common Transformer Core Stacking Methods
Direct or Butt-Lap Stacking
In a butt-lap structure, lamination sections meet at relatively direct joints.
Advantages:
- Simple arrangement
- Easier manufacturing
- Potentially lower production complexity
Limitations:
- Magnetic flux may cross a more concentrated joint gap
- Greater risk of localized flux distortion
- Magnetic performance can be less favorable than an optimized step-lap design
This method may be suitable for certain small or cost-sensitive transformers, subject to design requirements.
Step-Lap Stacking
A step-lap core distributes the joint across several successive layers. Instead of creating one concentrated discontinuity, the overlapping laminations provide a more gradual magnetic transition.
Potential benefits:
- Reduced flux concentration near the joints
- Lower localized saturation
- Lower excitation current
- Improved no-load performance
- Reduced core vibration and audible noise
The step dimensions and sequence must be engineered for the specific core. A fixed overlap of one-third of the sheet width is not a universal rule.
Step-lap joints are mainly intended to improve the magnetic path. Any thermal benefit is secondary and should not be represented as a fixed percentage without supporting test data.
Hybrid Stacking
A hybrid design combines different joint or stacking arrangements in selected areas of the core.
Potential advantages:
- Design flexibility
- Balance between manufacturing cost and magnetic performance
- Adaptation to special core geometries or production constraints
Because hybrid structures are more application-specific, their performance should be confirmed through engineering calculations and prototype or routine testing.
Which Stacking Method Produces the Lowest Core Loss?
A properly designed step-lap core will often offer better magnetic performance than a simple butt-lap structure. However, it is not accurate to guarantee that step-lap stacking will always reduce no-load loss by 15–20%.
The measured difference depends on:
- Electrical steel grade and thickness
- Core flux density
- Joint geometry
- Step-lap sequence
- Cutting and stacking tolerances
- Burr height
- Core clamping
- Transformer capacity and core shape
- Test conditions
Reliable performance claims should be based on comparable transformer designs, documented production data or witnessed test results.
Quality-Control Priorities
A dependable core-stacking process should include control at three stages.
Incoming Material Inspection
Verify the steel grade, thickness, coating, supplier documentation and material identification.
In-Process Inspection
Monitor cutting dimensions, burr height, lamination sequence, joint alignment, stack height and coating condition.
Final Verification
Inspect the completed core and perform the required transformer tests. Depending on the product and specification, these may include:
- No-load loss
- No-load current
- Applied-voltage testing
- Induced-voltage testing
- Insulation resistance
- Winding resistance
- Noise measurement
- Temperature-rise testing
Frequently Asked Questions
What is transformer core stacking?
It is the process of assembling insulated electrical steel laminations into the magnetic core of a transformer.
Why are thin laminations used?
Thin, mutually insulated sheets restrict circulating eddy currents and help reduce core heating and no-load loss.
What is a step-lap transformer core?
It is a core in which the joints are staggered across several lamination layers, creating a more gradual path for magnetic flux.
Is thinner electrical steel always better?
Not necessarily. Thinner steel can reduce eddy-current loss, but the final choice must also consider steel grade, total core loss, manufacturing capability, mechanical handling and cost.
How is transformer core quality verified?
Manufacturers combine material inspection, dimensional checks, process control, insulation verification and electrical testing of the completed transformer.
Conclusion
High-quality transformer core stacking requires more than placing electrical steel sheets together. It depends on verified materials, accurate cutting, a controlled lamination sequence, protected surface insulation, uniform clamping and documented inspection.
Step-lap construction can improve the magnetic path and support lower no-load loss, excitation current and noise. Its actual performance, however, must be evaluated as part of the complete transformer design rather than through isolated or universal percentage claims.
Request a Custom Transformer Solution
Need a transformer designed around your voltage, capacity, impedance, loss, cooling and installation requirements?
Dingxin — Power transformer manufacturer. Custom solutions are available.
Contact Dingxin to discuss your technical specifications and request a customized transformer proposal.
Table of Contents
- Why Is Transformer Core Stacking Important?
- Four Main Steps in Transformer Core Stacking
- How to Select Electrical Steel Laminations
- Why Material Batch Consistency Matters
- Three Common Transformer Core Stacking Methods
- Which Stacking Method Produces the Lowest Core Loss?
- Quality-Control Priorities
- Frequently Asked Questions
- Conclusion
- Request a Custom Transformer Solution